Turnkey Cleanroom Solutions Australia: Cost, Design, and Installation Guide
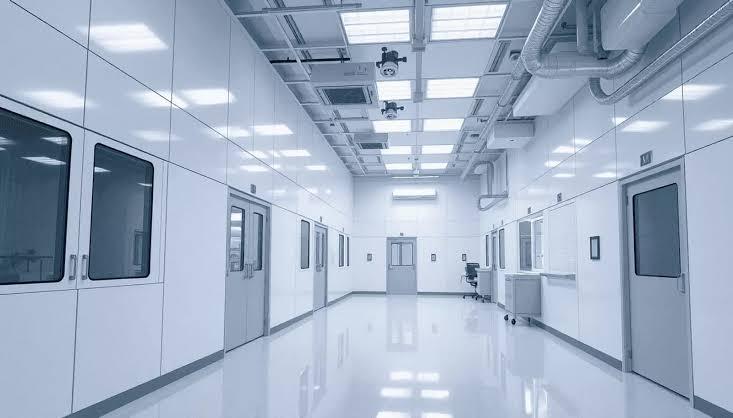
Getting a clean, certified manufacturing room off the ground anywhere in Australia is tough work. When you have to juggle strict TGA audit rules, tight ISO particle caps, and 42°C summer heatwaves, things get messy fast. The real trouble starts when you hire separate draftsmen, local AC mechanics, panel installers, and independent certifiers—trades blame each other, jobs sit idle, and original budgets go out the window. If your team is gearing up to formulate sterile injectables, assemble small satellite components, or build medical devices, waiting around for delayed sign-offs costs serious money every week. That is why turning to a single provider for Turnkey Cleanroom Solutions Australia takes the pain out of the build by combining architectural layout, specialized air handling, interior fit-out, and final compliance checks under one contract. Working alongside a dedicated team for Turnkey Cleanroom Solutions Australia ensures your air changes, room pressure differentials, and humidity controls hold steady through local heatwaves. Sourcing reliable Turnkey Cleanroom Solutions Australia protects your capital outlay from audit failures, while investing in proven Turnkey Cleanroom Solutions Australia gives your staff a dependable, ready-to-run clean space delivered right when promised.
Where Certified Cleanroom Environments Drive Innovation
Controlled environments form the quiet foundation of high-value Australian manufacturing, giving technical teams clean air and stable rooms to turn out delicate products.
Pharmaceutical, Biotechnology, and Sterile Compounding
Biotech labs and sterile fill suites rely on steady positive air pressure, HEPA airflow curtains, and seamless wall joints to stop airborne microbes in their tracks. Investing in dedicated Turnkey Cleanroom Solutions Australia ensures your facility satisfies PIC/S cGMP and TGA requirements without costly revisions. Implementing certified Turnkey Cleanroom Solutions Australia prevents cross-contamination between sensitive processing suites, while working with a top-tier provider of Turnkey Cleanroom Solutions Australia keeps high-volume manufacturing lines operational day after day. Equipping your facility with high-end cleanroom technology safeguards sensitive biological batches, while precision HVAC maintains unyielding temperature and relative humidity stability year-round.
Advanced Semiconductor, Defence, and Aerospace Labs
Local space startups and defense optics labs need cleanrooms from ISO Class 5 to Class 8 to mount circuit boards, handle specialised lenses, and test satellite instruments without dust specks or static shocks ruining fragile assemblies.
Cleanroom Cost, Design, and Installation Factors
Building a compliant cleanroom in Australia means balancing your available capital against outdoor weather swings and durable materials:
1. Estimating Capital Costs (CAPEX vs. OPEX)
Cleanroom projects across Australia usually land somewhere between AUD $2,500 and AUD $10,000+ per square meter. That price depends heavily on the cleanliness level you need (ISO 5 through ISO 8) and your regulatory bracket (TGA Grade A down to Grade D). Working with a turnkey builder prevents mid-project budget blowouts by bundling design, materials, and on-site trade work into one fixed quote.
2. Specialised HVAC Design for the Australian Climate
Australia sees harsh weather swings, from 40°C summer scorchers to damp coastal humidity. A proper cleanroom HVAC setup uses terminal HEPA/ULPA filters, dedicated desiccant dehumidifiers, and intelligent control software to hold tight humidity and temperature bands without running up massive energy bills.
3. Modular Architectural Wall and Ceiling Panels
Flush modular panels built with aluminium honeycomb or fire-safe rockwool cores come finished with chemical-resistant coatings. They stand up easily to harsh wipe-downs with vaporised hydrogen peroxide (VHP) and eliminate ledges where dust might settle.
4. Turnkey Installation and Rapid On-Site Assembly
Prefabricated panels and pre-tested mechanical skids arrive on site ready to bolt together. This cuts on-site installation timelines by up to 40% compared to messy plasterboard and drywall construction.
Key Benefits of a Single-Source Turnkey Approach
Hiring one team to deliver your cleanroom from start to finish brings clear perks over trying to manage half a dozen separate sub-trades:
- One team owns the outcome: From the first floor layout to the final signed test sheet, one builder takes full responsibility for passing audits.
- Clear upfront costs: Ironing out the mechanical and air design before cutting panelling keeps change orders low and stops surprise invoices later on.
- Much faster project turnarounds: Building panels and air systems off-site while prepping the building slab knocks months off the build calendar.
- Straightforward compliance paperwork: Ready-to-go Design Qualification (DQ), Installation Qualification (IQ), and Operational Qualification (OQ) templates make TGA and ISO reviews painless.
- Sensible long-term power bills: Variable-speed fan filter units and efficient chillers help keep continuous power draws aligned with NCC Section J energy rules.
Our Simple 4-Step Turnkey Delivery Process
Getting your clean space built should feel organized, straightforward, and clear from the very first meeting:
Step 1: User Requirement Brief & Engineering Layout
We sit down with your engineers to review process flows, airlock locations, equipment weights, and target ISO clean bands, sketching them directly into clear 3D layout drawings.
Step 2: Off-Site Precision Fabrication
Wall panels, walkable ceiling grids, interlocked pass-through boxes, and pre-piped air skids are manufactured under controlled conditions so everything slots together neatly on site.
Step 3: Fast-Track Clean Build & Customized Mechanical Fit-Out
Our specialist installers erect the modular envelope, hang ductwork, seal terminal HEPA filters, and wire up customized monitoring controls without unnecessary delays.
Step 4: Testing, Air Balancing & Final Validation
We run comprehensive particle counts, airflow visualization smoke tests, pressure differential checks, and recovery time tests, handing over a complete IQ/OQ compliance binder.
Proven Fit Across Industrial and Research Facilities
Modular cleanrooms adapt well to different manufacturing footprints across the country:
Private Medical Laboratories & Biotech Scale-Ups
Young biotech startups and pilot labs get practical modular suites that can be lengthened, partitioned, or rearranged as production scales from trials into commercial supply.
Commercial Cleanroom Fleets & Multi-Suite Campuses
Large contract manufacturing organizations (CMOs) get interconnected clean suites, automated personnel airlocks, and central plant rooms built for high daily output with minimal downtime.
Why Australian Innovators Choose Our Turnkey Services
Picking a cleanroom builder comes down to technical know-how, local regulatory experience, and having a team that stays on the job until every test passes.
We build modern modular cleanroom systems engineered to perform reliably through Australian summers while staying fully compliant with global cGMP and ISO standards. When life sciences organizations search for a dependable Turnkey Cleanroom Solutions Australia provider, they trust our straightforward communication and meticulous execution. Working with our Turnkey Cleanroom Solutions Australia team gives facility directors direct access to senior cleanroom engineers who understand room pressure cascades and airflow dynamics inside and out. Engaging our dedicated Turnkey Cleanroom Solutions Australia crew ensures your facility passes its final validation tests smoothly, backed by comprehensive parts and workmanship warranties.
Bring Your Cleanroom Project to Life on Time and on Budget
Do not let contractor miscommunication, complex HVAC specs, or shifting compliance rules push back your facility opening. Your scientific work and high-precision products deserve a clean environment that performs reliably right from day one.
When you want honest pricing, dependable schedules, and proven cleanroom engineering, trust the turnkey Cleanroom Solution provided by Pod Tech Company. Get in touch with our Australian engineering team today to review your project brief, walk through layout options, and build a cleanroom facility built around your exact production needs.
Frequently Asked Questions
1. How long does a turnkey cleanroom build take in Australia?
A modular cleanroom generally takes 12 to 24 weeks from approved drawings to final validation sign-off. That is significantly faster than traditional drywall builds, which routinely drag out past 12 months due to trade delays.
2. What is the difference between ISO Class 7 and ISO Class 8 cleanrooms?
An ISO Class 7 space allows no more than 352,000 particles (≥0.5 µm) per cubic meter of air and typically runs 30 to 60 air changes per hour. An ISO Class 8 room permits up to 3,520,000 particles per cubic meter and requires around 10 to 25 air changes per hour.
3. Does a turnkey cleanroom contract include TGA or ISO validation?
Yes. A proper turnkey package includes full validation documentation—Design Qualification (DQ), Installation Qualification (IQ), and Operational Qualification (OQ)—as well as on-site particle counting, filter integrity testing, and room pressure balancing.
4. Can modular cleanroom walls be reconfigured or expanded later?
Yes. Modular cleanroom panels, walkable ceilings, and fan filter units can be unbolted, relocated, or expanded with minimal disruption and almost zero dust, making them ideal for growing facilities.
Thanks- Iyabook.com for publising this blog!

 English
 Arabic
 French
 Spanish
 Portuguese
 Deutsch
 Turkish
 Italiano
 Russian
 Romaian
 Portuguese (Brazil)
 Greek